


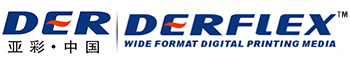
PVC Fabric for Automated Truck Curtain Manufacturing
PVC coated polyester rolls selected for the realities of automated trailer curtain production: repeatable feeding, controlled joining, usable width, reinforcement bonding and optional fleet graphics. DERFLEX supports fabricators and trailer-cover manufacturers with a specification-first approach to material trials and repeat roll orders. Submit your line type, seam geometry and inspection criteria so the material can be evaluated on your equipment before volume release.
01 / PRODUCTION FIRST
Automated truck curtain production requirements
The correct fabric is not simply the heaviest PVC sheet. It is a repeatable roll material that feeds predictably, bonds to specified seam and reinforcement constructions, and remains consistent from approval roll to later production lots.
What an automated line needs
Automated curtain-side fabrication converts a moving web into multiple long panels. Unexpected edge waviness, blocking between layers or changes in coating behavior can interrupt registration, cutting, welding and downstream reinforcement attachment. Converters should specify the unwind direction, tension window, edge trim and roll identification alongside mechanical strength.
For side-curtain manufacturers, fabric selection also affects folded curtain behavior, buckle zones and visual uniformity of fleet-branded panels. A good trial mimics the largest intended panels, the smallest seam overlap, and the actual production speed rather than relying only on a handheld bond demonstration.
02 / MATERIAL ENGINEERING
PVC coating, base fabric & welding compatibility
The polyester base cloth carries much of the mechanical load; the PVC coating enables weather resistance and thermoplastic joining. Coating recipe, finish and joining parameters need to be checked together.
Build your seam qualification around the actual construction
For an automatic truck curtain welding fabric, record coating side orientation, overlap width, electrode or hot-air head geometry, process speed, applied energy or temperature, pressure and cooling time. Then evaluate the resulting bond with a repeatable peel or shear method appropriate to your product.
Screen weld appearance at starts, stops, corners and reinforced intersections. Keep the sample conditioning period and test direction consistent; process settings from one fabric finish should not automatically be transferred to another.
Explore DERFLEX PVC coated truck side curtain material and broader PVC coated fabric manufacturing options before specifying your test grade.
Base fabric
Agree on polyester yarn structure, tensile and tear methods, dimensional stability and intended load paths. Do not infer curtain-system strength from yarn denier alone.
PVC compound
Evaluate coating adhesion, flexibility, surface friction and blocking after storage. Confirm whether lacquer or surface treatment affects the chosen joining method.
Weld process
Check hot-air, hot-wedge or high-frequency welding separately. Approve sample settings and acceptable bond performance before scaling production.
03 / ROLL CONTROL
Roll flatness, usable width & tension
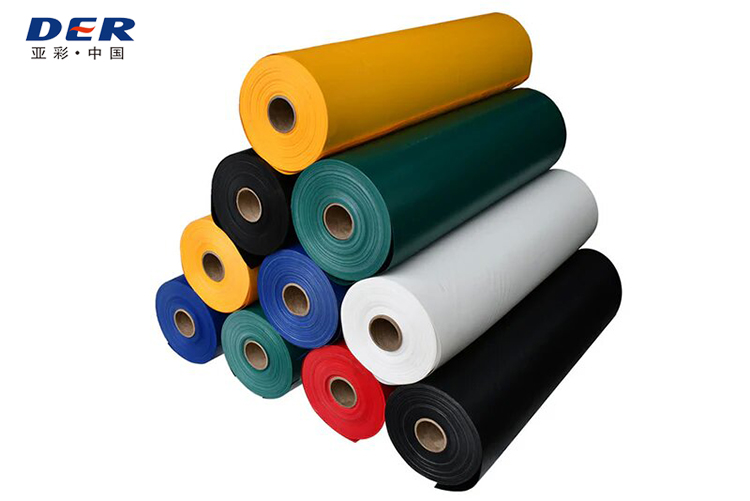
A nominal 3.2 m roll is not necessarily 3.2 m of usable material. Your purchasing specification should define what the line can cut and join after allowed edge trimming, not only what appears on the supplier label.
Measure the web where it matters
Inspect flatness across the web and along the roll after a defined relaxation period. Document edge curl, telescoping, wrinkle or crease acceptance, coating defects, winding tightness and the distance reserved for edge trim. Feed stability can change with roll diameter, winding direction, line speed and ambient conditions.
Specify whether width is measured from coated edge to coated edge or only between accepted edges. Agree on how frequently measurements are taken and whether tolerances apply per roll or per lot. See fabric supplied by the roll and the industrial PVC fabric portfolio for related converter materials.
| Variable | What the converter should specify | How to verify |
|---|---|---|
| Nominal / usable width | Both widths, edge exclusion and permitted variation | Across-web measurements at agreed locations |
| Roll length & joints | Target length, acceptable short rolls, splice rules | Roll log and physical unwind check |
| Flatness / edge curl | Acceptable waves, creases, curl or bow under defined conditions | Inspection on representative unwind length |
| Winding & core | Coating-in/out direction, core ID, roll OD / mass limits | Label and reel-handling inspection |
| Tension / tracking | Line speed, tension operating range and registration expectation | Recorded production trial on target equipment |
| Coating / appearance | Color, gloss, finish, visual defect limits and lot variation | Approved master swatch and batch records |
| Identification | Grade, lot, roll number and packing record fields | Label-to-certificate traceability check |
04 / DOWNSTREAM FABRICATION
Reinforcement & print compatibility
Truck curtain production adds more than a continuous field seam. Straps, patches, hems and printed graphics must remain compatible with the finished coated surface and the chosen joining sequence.


Reinforcement zones
Define webbing material, patch orientation, stitch or weld pattern, required overlap and edge distance around buckle points and closures. A weld that looks sound in a flat strip may fail differently around multi-layer corners or hardware attachment points. Include full-stack samples in the trial.
Material choices for high-contact areas are discussed in abrasion-resistant curtain fabric and truck-side curtain tarpaulin programs.
Graphics and surface treatment
If the finished side curtains carry fleet branding, qualify ink adhesion, print durability, color, gloss and the clearance between printed artwork and welded edges. UV, solvent, eco-solvent or other print processes should not be assumed compatible without testing the exact lacquer and ink system.
Additional context is available in truck side curtain fabric specifications.
05 / SAMPLE VALIDATION
Trial test checklist & sourcing specifications
Request a defined sampling window: material and documentation should arrive before the line trial, results should be captured with clear acceptance criteria, and the approved roll lot should be retained as a reference for future shipments.
Suggested production-line trial sequence
- Agree on the target design. Provide curtain height, panel widths, planned seams, reinforcement zones and sample quantities.
- Confirm roll acceptance. Inspect usable width, web appearance, labels, core, winding and packing before feeding the machine.
- Record the line setup. Log machine type, welding head / electrode, overlap, line speed, pressure and energy or temperature.
- Test the difficult transitions. Include starts, stops, corners, attachments, patches and any print-to-weld margins.
- Evaluate and sign off. Record seam failure mode, peel/shear outcomes, visual defects, feed stability and any required environmental conditioning.
- Freeze the purchase reference. Approve the retained sample, inspection methods, roll tolerance schedule and lot labeling.
Trial duration and sample quantity are agreed per project; this is a proposed qualification workflow, not a promised factory test service or a published numeric guarantee.
| Check | Record | Decision basis |
|---|---|---|
| Feed stability | Wrinkles, lateral drift, tension, stoppages | Meets approved trial criteria at target speed |
| Weld quality | Settings, overlap, bond test results, failure mode | Meets agreed seam test and visible finish criteria |
| Reinforcement | Patch and webbing bond, corner stress points | Approved whole-assembly performance |
| Print compatibility | Ink system, adhesion and finish observations | Approved ink / surface combination |
| Roll quality | Usable width, edges, splices, winding, labels | Matches signed roll specification |
| Repeat orders | Batch ID and retained reference sample | Accepted against agreed QC protocol |
06 / PROCUREMENT DECISION
Why converter-grade sourcing is different
Online finished-tarp buying
Usually begins with a predefined cover size and a ready-made finished product. It may not specify roll flatness, splices or production-line behavior.
Generic PVC roll sourcing
Often compares nominal GSM, width and price per meter, but may leave welding method, usable width and batch traceability unresolved.
Automated line sourcing
Starts from cutting yield, machine compatibility, seam qualification and controlled repeat orders. Acceptance needs agreed evidence rather than a catalog claim.
How DERFLEX fits the project
DERFLEX offers PVC coated polyester fabric options for truck curtain fabrication and industrial roll supply. The correct next step is a line-specific sample and written agreement on construction, process compatibility and roll controls—not a blanket promise that one roll suits every automated welding platform.
For alternative finished-product and supply models, compare OEM truck side curtains and industrial coated fabric rolls.
07 / BUYER QUESTIONS
Frequently asked questions
What PVC fabric is suitable for automated truck curtain welding?
Start with double-side PVC coated polyester fabric specified for the intended hot-air, hot-wedge or high-frequency joining method. Approve the actual coating finish and an overlap seam on your production line; nominal GSM alone does not establish weldability.
How do I specify usable roll width rather than nominal width?
State the minimum usable coated width after excluding edge defects, and agree on the measurement method, inspection points and acceptable edge trim. Match that width to your cutting layout and seam plan.
Can one truck curtain fabric work with both HF and hot-air welding?
Some PVC coated fabrics can be processed by both methods, but a successful result depends on formulation, surface finish, tooling, overlap geometry and machine settings. Qualify each process separately using sample rolls.
What should a trial roll evaluation include?
Record unwind behavior, edge curl, flatness, tracking, roll joints, seam appearance, peel and shear results, reinforcement bonds, print adhesion where applicable and lot identification. Compare results with written pass/fail criteria.
Are welded truck curtain seams automatically waterproof?
No. Fabric water resistance does not prove that every seam, stitch, hole or hardware interface is watertight. Test finished seam assemblies and representative reinforced areas under the intended use conditions.
What should I send for a factory quotation?
Share desired GSM and fabric construction, nominal and usable width, roll length, core and winding direction, joining process, line speed, seam geometry, printing finish, trial quantity, target delivery location and acceptance tests.
YOUR PRODUCTION LINE / OUR MATERIAL DISCUSSION
Request PVC Fabric Samples for Your Truck Curtain Production Line
Tell us the joining technology, target usable width, production speed, preferred coating finish and intended order volume. Include a seam drawing or current fabric sample if available. Our team can review the requested material direction and quote the applicable supply scope.
Send with your enquiry
Machine and joining process · seam geometry · GSM / base cloth · nominal and usable width · roll length · reinforcement and printing requirements · required tests · destination
Request Samples & Quote